Direct factory procurement solutions engineered under ISO 13485 and CE standards. Batch-tested for pressure integrity, leak resistance, and biocompatibility.
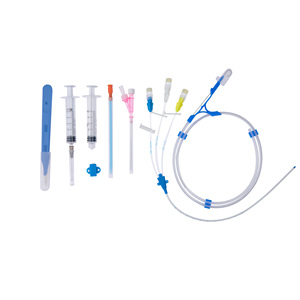
Understanding polymer selection, pressure rating validation, and ISO 80369-7 compliance when procuring fluid management components for critical care and infusion therapy.
In modern clinical fluid dynamics, the medical 3-way stopcock valve serves as the fundamental nexus for intravenous (IV) therapy, hemodynamic pressure monitoring, anesthesia delivery, and oncology drug administration. As hospital procurement committees and original equipment manufacturers (OEMs) streamline supply chain risk, China has established itself as the world’s primary industrial hub for precision injection-molded fluid control devices. However, navigating the ecosystem of Chinese stopcock valve manufacturers requires a deep technical evaluation beyond initial unit pricing.
The manufacturing of medical-grade stopcock valves demands strict mechanical tolerances. A variance of less than 0.01 millimeters in the taper angle of a Male or Female Luer lock can lead to micro-leakages, air embolism risks, or environmental exposure to hazardous chemotherapy agents. Leading Chinese factories have shifted from standard commodity molding to automated, high-precision robotics utilizing specialized medical-grade polymers, such as lipid-resistant Polycarbonate (PC) and polysulfone blends.
This whitepaper provides procurement executives, clinical engineers, and OEM brand owners with a comprehensive, empirical evaluation framework for sourcing stopcock valves and related catheter accessories from premier Chinese manufacturing facilities. By analyzing material science advancements, pressure rating testing, cleanroom quality management systems (QMS), and regulatory dossier compliance, buyers can establish high-yield, zero-defect supply chains.
Utilizing certified lipid-resistant Polycarbonate prevents environmental stress cracking (ESC) caused by intravenous fat emulsions, oncology therapeutics, and volatile anesthetics.
Full conformance to small-bore connector standards ensures universal fluid interchangeability without risk of misconnection or back-flow leakage under pressure.
Terminal EO sterilization cycles with residual testing below ISO 10993-7 thresholds guarantee sterile product delivery with zero chemical toxicity.
The global fluid management landscape is undergoing rapid innovation. Key trends shaping procurement decisions include lipid resistance, automated assembly, and high-pressure ratings.
Standard Polycarbonate (PC) stopcocks have historically been susceptible to Environmental Stress Cracking (ESC) when exposed to lipid solutions (e.g., Total Parenteral Nutrition, propofol infusions, and alcohol-based drug formulations). When lipids penetrate the polymer micro-structure, internal molecular bonds weaken, resulting in catastrophic hub cracking and fluid leaks. Top-tier Chinese manufacturers now formulate proprietary lipid-resistant PC grades that maintain tensile strength and transparency even after 72 hours of continuous lipid exposure.
With the rise of minimally invasive interventional radiology and contrast-enhanced imaging, standard low-pressure IV stopcocks (typically rated at 4.5 to 7 PSI) are insufficient. Global buyers are increasingly sourcing specialized high-pressure 3-way stopcocks rated from 200 PSI up to 1,200 PSI. These valves incorporate reinforced body walls, modified high-density polyethylene (HDPE) handles, and dual silicone O-ring internal seals to withstand power injection of viscous radio-opaque contrast media.
Labor-intensive manual insertion of handles into stopcock bodies introduces human variability, potential particulate contamination, and inconsistent turning torque. Industry-leading Chinese factories have installed fully automated robotic assembly lines operating inside ISO Class 7 cleanrooms. Integrated high-speed machine vision cameras inspect 100% of units for body flash, luer thread integrity, handle alignment, and foreign particulates prior to inline pressure testing.
Occupational exposure to hazardous oncology drugs has forced clinical guidelines to mandate closed fluid pathways. OEM manufacturers are redesigning stopcock bodies to integrate needleless access ports, swabable valves, and rotational luer-lock collars directly into the valve housing, reducing dead space volume to less than 0.05 mL.
| Material Component | Standard Resin | Advanced Resin (Recommended) | Clinical Advantage | Pressure Rating Limit |
|---|---|---|---|---|
| Valve Body | Standard Medical Polycarbonate | Lipid-Resistant Polycarbonate / Polysulfone | Eliminates stress cracking with lipids & oncology drugs | Up to 1,200 PSI (High Pressure) |
| Rotating Handle | Standard Polyethylene (PE) | High-Density Polyethylene (HDPE) / ABS | Smooth turning torque, non-binding rotation | 4.5 to 500 PSI |
| Internal Seal / Ring | Natural Rubber / PVC | Medical Silicone (Platinum-Cured) | DEHP-free, zero cytotoxic leaching, leak-tight fit | Up to 1,200 PSI |
| Extension Tubing | Plasticized PVC | DEHP-Free PVC / Polyurethane (TPU) | High kink resistance, biocompatible fluid pathway | Up to 300 PSI |
Direct-from-factory procurement grants international distributors, OEM partners, and hospital groups unmatched technical control, cost efficiency, and quality assurance.
Full CE Marking, ISO 13485 QMS certification, WHO-GMP compliance, and FDA 510(k) supporting technical files enable rapid regulatory clearance in EU, LATAM, and US markets.
Complete private-label manufacturing: customized handle colors (blue, red, white, yellow), clear or translucent bodies, integrated extension tubing lengths (10 cm to 150 cm), and sterile blister printing.
Equipped with modern Swiss-machined injection molds, optical automated dimensional inspection, hydraulic burst testing rigs, and automated residual EO gas chromatography analyzer labs.
To ensure total risk mitigation, international buyers should execute the following 5-step verification process when auditing Chinese stopcock valve suppliers.
Our engineering team delivers full product specification sheets, ISO certificates, and free sample kits for prospective medical device distributors and hospital tenders.
Direct answers to common questions asked by international procurement managers, regulatory directors, and OEM buyers.
Standard 3-way stopcocks are molded from general-grade Polycarbonate, which can develop micro-fractures (crazing) when exposed to lipid emulsions, alcohol solutions, or chemotherapy agents. Lipid-resistant stopcocks utilize advanced polymer formulations that withstand chemical stress cracking, ensuring fluid pathway integrity during prolonged infusion of parenteral nutrition or lipid-soluble pharmaceuticals.
Yes. All male and female luer lock connectors manufactured by our partner facilities are fully compliant with ISO 80369-7 standards for small-bore connectors for intravascular applications. This guarantees universal fitment, precise fluid sealing, and prevention of misconnection with non-vascular systems.
We supply stopcocks across multiple clinical pressure tiers: Standard Low-Pressure Stopcocks (rated up to 4.5 bar / 65 PSI for gravity IV administration), Medium-Pressure Stopcocks (rated up to 200–300 PSI for pump-driven infusions), and Ultra High-Pressure Stopcocks (rated up to 1,200 PSI for angiography and CT contrast media injection).
Absolutly. OEM and private-label programs support custom tube lengths (e.g., 10 cm, 25 cm, 50 cm, 100 cm, 150 cm) with or without needleless injection sites. Rotation handle color options include clinical standard Blue (venous), Red (arterial), Yellow, and White for clear line identification.
Every shipment is accompanied by batch Certificate of Analysis (CoA), ISO 13485 QMS documentation, CE Declaration of Conformity, WHO-GMP certificate, Ethylene Oxide sterilization validation reports, and ISO 10993 biocompatibility testing data (cytotoxicity, systemic toxicity, sensitization).
For standard sterile blister-packed stopcock valves, MOQ starts at 5,000 to 10,000 units. For custom OEM formulations or private-label printed pouches, MOQ is typically 20,000 units. Production lead times range from 15 to 25 days depending on tooling and sterilization validation schedules.